At Glanbia Ireland, a casein powder dryer ran deliberately below its final moisture specification. Continuous measurement in granular powder was difficult, and the plant preferred a moisture comfort margin to the risk of wet, off-spec product. A published case study describes how a real-time estimate helped recover some of that margin and increase production, although its results are vendor-reported.
An AI soft sensor estimates a hard-to-measure property from available process signals, such as temperatures, pressures, flows and previous laboratory results. AI soft sensor solutions bring that information forward in time; they do not make the laboratory reference unnecessary. At a fictional mid-size whey and milk-powder plant in Centre-du-Québec, QA manager Nadia may receive an hourly moisture result after bagging.
Engineering wants a continuous estimate of final moisture and eventually wants to use it to steer the dryer. Nadia owns the reference test and product hold and release decisions. Raising the moisture target could reduce unnecessary drying, but it also narrows the room for variability and prediction error. The question is how that estimate earns authority without becoming an unverified quality decision.
A moisture comfort margin protects quality but consumes saleable product
The current margin is not simply a conservative habit. It compensates for the uncertainty between making powder and receiving evidence about what was made. That protection sets the limit on what can be recovered.
The upper limit is only useful when variability is controlled
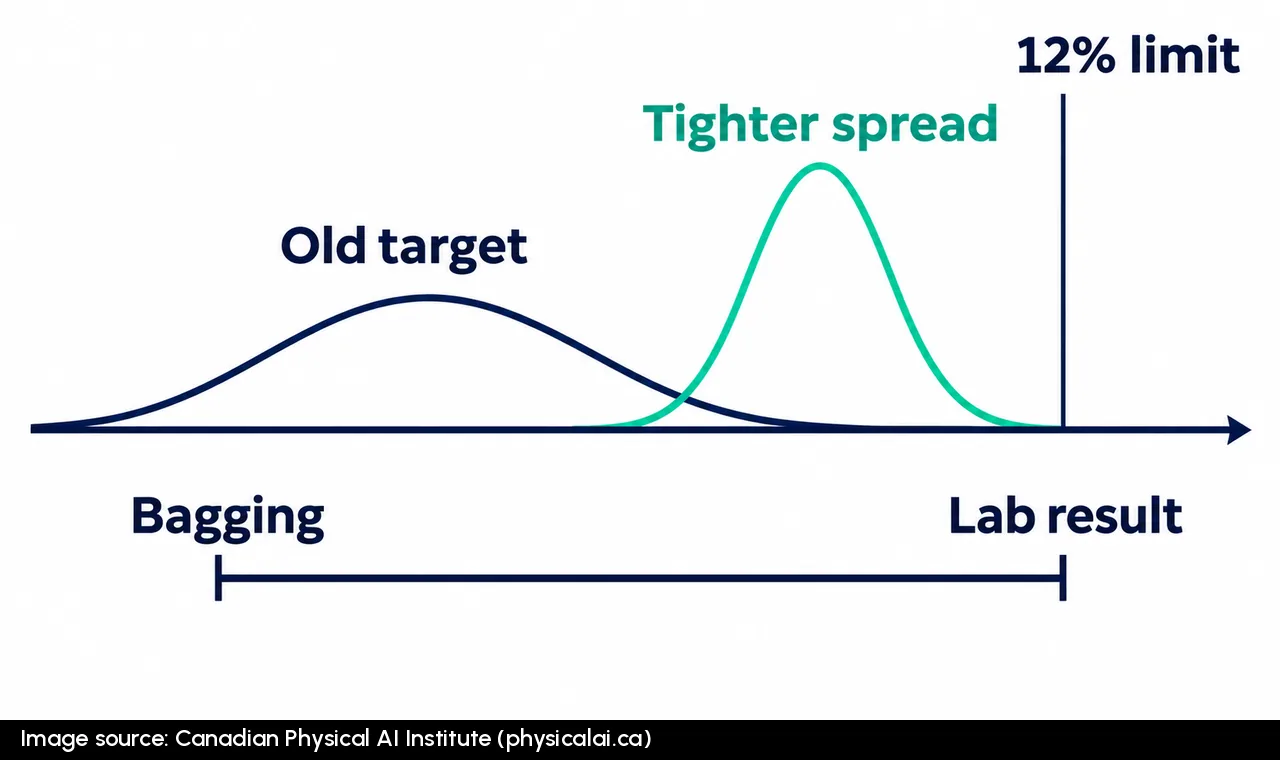
In the Glanbia case, final moisture had a 12% specification limit, yet the dryer ran well below it. Moving closer risked blockages in the dryer, cyclones or mill, and an off-spec batch might need to be sold at a discount. The target covered both product variation and delayed confirmation.
That margin also carried a production cost. With the same dry solids, removing extra water lowers finished powder mass, while the dryer uses capacity and energy to remove moisture the specification permits. Engineering sees an opportunity to raise average moisture; QA sees the associated upper tail of the distribution. Neither view is complete without the other.
Lower variation creates room to move the target
The case used an inferential moisture measurement inside model predictive control, combining raw-material quality, dryer air temperatures, operating settings and laboratory results. Better control of variation made a higher average moisture target more practical, rather than merely providing a faster number on a screen. The potential gains were both retained water in the product and dryer capacity freed for additional production.
A continuous prediction helps only when its relationship to actual moisture is understood near the specification boundary. That begins with what the software measures indirectly and how it learns to do so.
 Reader offer · ends November 11Where is the hidden cost in your factory?Watch it with 3 months of Premier free →
A soft sensor learns the relationship between process signals and a delayed result
Nadia already has temperatures, airflow, feed measurements and dryer operating history. She lacks the timely finished-moisture result, and algorithm choice alone cannot provide reliable estimates.
An inferential sensor uses measurements the plant already has
Also called a virtual or inferential sensor, a soft sensor learns the relationship between available measurements and a reference result. For a powder dryer, its inputs might include inlet and outlet air conditions, feed rate and properties, operating settings and historical moisture tests. It then estimates the delayed property from current data.
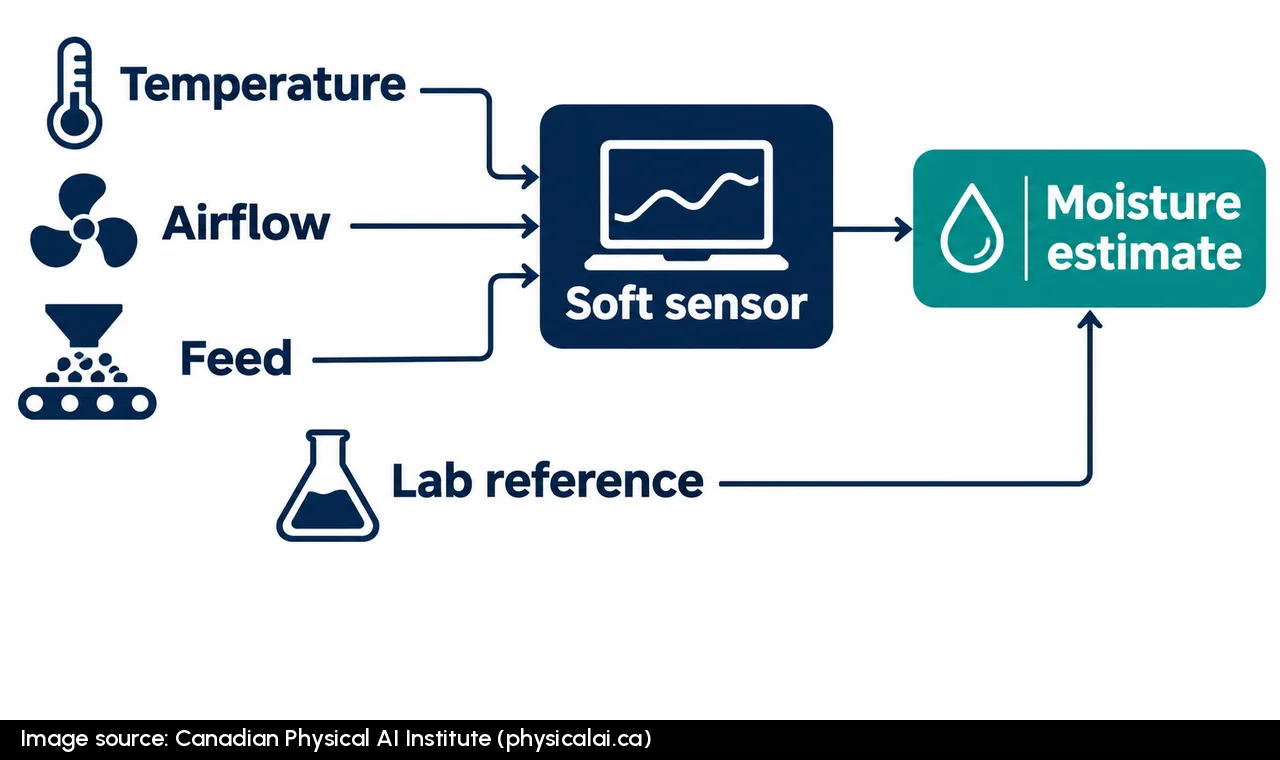
An AI sensor uses a learned model to interpret measurements or estimate a property; it may combine software with physical instrumentation rather than being a new physical measuring device. In this article, the AI soft sensor estimates powder moisture from existing dryer signals and laboratory references.
Linear regression, partial least squares, neural networks and models combining physics with statistical learning can all serve this purpose. A simple model may work under stable, approximately linear conditions; a more complex one may capture interactions and process history but become harder to inspect. The review by Kadlec, Gabrys and Strandt identifies missing values, noise, correlated signals, different sampling rates and changing conditions as recurring problems. Complexity cannot repair poor data.
An existing instrument can replace an expensive dedicated measurement
A different food process shows why reusing installed instrumentation can matter. At Frito-Lay, machine learning used images from an existing vision system to estimate potato weight against conveyor-weigher references, according to a trade press implementation account. Dedicated weighing elements cost approximately $300,000 per line, whereas the image-based mass-flow estimate required no additional camera hardware. The company had 35 such production lines in the United States alone.
Avoiding new weighing hardware does not eliminate development, integration or maintenance costs. For Nadia, the parallel choice is whether to buy dedicated continuous moisture instrumentation or derive a trustworthy estimate from installed signals. Either route still depends on reference measurements against which the result can be checked.
Neither a physical sensor nor a soft sensor is universally better: the choice depends on measurement feasibility, delay, maintenance, accuracy and the consequences of error. A soft sensor can provide earlier estimates, while a suitable physical reference remains essential for checking performance and supporting QA decisions.
Process knowledge can improve the model’s structure
Existing data becomes more useful when the model reflects how material and energy move through the dryer. An ongoing Danone and TU Delft research project models the chamber, fluid beds, cyclone and fines-return system in a multistage infant-formula dryer, together with recent operating history. It aims to estimate moisture and tapped density, and early findings suggest equipment connections help represent mass and energy flows. Local agglomeration near the nozzle remains difficult to capture.
This is ongoing research, not commercial control evidence. It suggests that treating measurements from interacting dryer stages as unrelated inputs can lose useful structure. Even a well-structured model, however, needs evidence that earlier moisture information can change production outcomes.
Published dryer cases show production gains, but not automatic QA authority
Operating cases show potential control benefits under specific conditions, not permission for AI to release product. Laboratory reference and model support remain part of the arrangement.
Glanbia recovered moisture margin and operating time
The Glanbia implementation took 12 weeks, according to the published account. Its vendor-reported results included a 0.65% increase in mean moisture, approximately seven additional hours per week of on-spec production through better start-up control, and investment recovery within four months. Performance was reportedly sustained through an ongoing support programme, an important part of the economics rather than an incidental footnote.
Those outcomes support a case for improved dryer operation, reduced moisture giveaway and capacity recovery. They do not establish independent release authority or predict Nadia’s payback.
Four Australian milk-powder dryers show the value of frequent prediction
At Murray Goulburn, a published account describes moisture-related process data collected every 15 seconds across four milk-powder dryers. An operator also sampled powder hourly with an infrared instrument, feeding those results back to adjust the model. This pairing supplied frequent estimates between physical checks rather than replacing the checks themselves.
The vendor-reported outcomes were a 52% average reduction in moisture variability, about one additional tonne of powder per day across the four dryers, and an energy reduction contributing another 5% to 10% to return on investment. They describe process performance, not independent QA release authority. More importantly for Nadia, the case makes feedback from real samples part of the control design.
Other deployments show why the benefit depends on the process
The range of results widens in a Northern European milk-producer case covering closed-loop inferential moisture control on three caseinate spray towers. Vendor-reported outcomes included up to 42% lower quality variability, moisture increases of 0.12 to 0.38 percentage points and throughput gains of 6% to 15.8%. The spread matters because the constraint, equipment and starting variability determine what improvement is available.
A 2025 industrial sugar crystallization study provides a related but different example: machine learning predicted Brix from control data, with a reported 2.12% decrease in mean crystallization residence time. That is an industrial research result, not a vendor dryer outcome, and it does not validate dairy moisture or release decisions. The dryer figures also come without a published independent audit. The cases establish plausible mechanisms, not guaranteed returns, which makes target selection more important than copying reported gains.
The best prediction target is one that changes an operating decision
Once the opportunity looks credible, Nadia still has to decide what to predict first. The useful target is not necessarily the laboratory property with the largest historical dataset. It is one that influences action while material remains controllable.
Moisture has a direct connection to dryer settings and finished mass
Final moisture offers a direct link between dryer conditions, finished powder mass and specification risk. A timely estimate can warn of movement toward a limit while an adjustment remains possible. The pilot can test predictions against matched laboratory results, not just an abstract model score.
Timing belongs in that test. A highly accurate estimate produced after the corresponding powder leaves the dryer offers little control value. Moisture suits this dryer, not necessarily every plant.
Viscosity and texture require a more precise target
A sauce may satisfy a laboratory viscosity method yet behave differently at a filler because temperature and shear are different. Likewise, an extruded food can meet moisture requirements while missing the desired texture. QA and engineering need to distinguish reproducing a test from predicting a failure.
A laboratory viscosity estimate is not the same as a warning about unstable filling, just as texture measurement differs from the risk of leaving a validated extrusion window. Powder moisture and tapped density are also separate targets, as the spray-drying research illustrates. Combining them into a vague quality score would make both validation and action harder to define, so Nadia keeps tapped density outside her first pilot.
Brix and fill consistency need different responses
In crystallization, Brix prediction can inform the timing of a process endpoint. In filling, a useful estimate might instead concern product behaviour contributing to underfill, overfill or inconsistent delivery, helping distinguish changing material properties from a mechanical fault. They require different interventions.
Before treating filling as a prediction problem, the plant can examine mechanical faults, checkweigher feedback and product-condition variation separately. Our guide to reducing filler giveaway explains those alternatives. Nadia keeps the pilot focused on the dryer.
Fouling changes what the model can observe
Even with moisture as the target, the input measurements can fail before the product goes out of specification. A coated window or drifting probe may corrupt a signal, while physical fouling can change heat transfer and the relationship between feed conditions and finished moisture. The first problem calls for restoring measurement quality; the second can invalidate the learned relationship itself.
An anomaly detection approach may flag unusual behaviour but cannot, by that alert alone, identify whether the source is an instrument, the equipment or the product. When a prediction and laboratory result disagree, the right response starts by establishing which material and time each number represents.
A disagreement with the laboratory starts with the batch timeline
The current prediction and the latest lab report may describe different powder, confusing delay with error. Nadia needs a record that links the sample to the conditions under which that material was made.
The golden batch timeline separates sampling from reporting
A golden batch timeline ties each physical sample to its lot, product, recipe version, relevant process conditions, operator changes, cleaning status and final disposition. It distinguishes when the material experienced those conditions, when the sample was actually collected and when the result became available. Those three timestamps let engineering retrieve the prediction that corresponds to the sample rather than the current on-screen number.
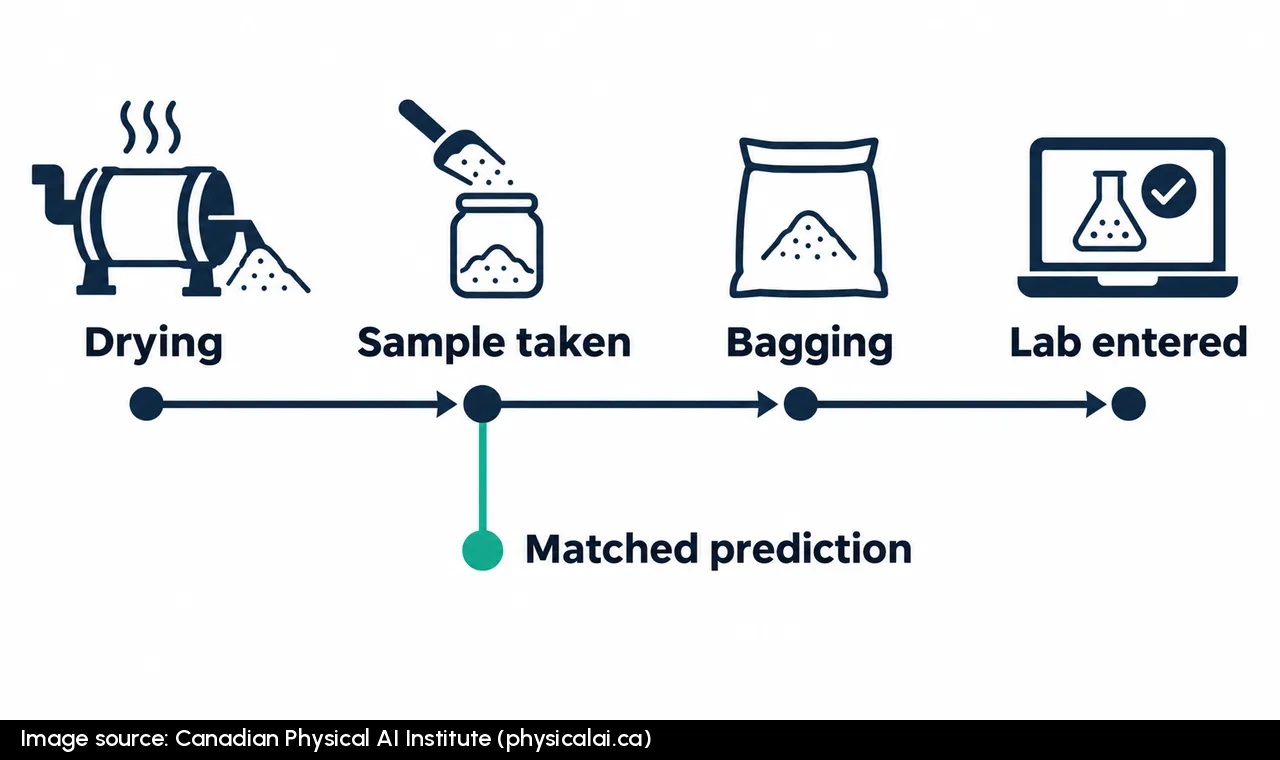
Practitioner guidance on inferential monitoring warns that laboratory information systems sometimes record a scheduled time instead of the actual collection time. Misalignment can make a sound model appear poor, or a poor model appear accurate, especially during transitions. Our article on manufacturing AI data foundations explains why joined records matter before model development.
The laboratory reference has its own uncertainty
Even a correctly matched sample can disagree because collection, transfer and analysis introduce error. A chemical-plant practitioner account reports that an engineer at SABIC Gelsenkirchen attributed roughly 95% of observed laboratory bias to the laboratory process, including analysis practices, sample transfer and residue in sample ports after grade changes. That was one engineer’s assessment, not a measured rule for dairy laboratories.
The lesson is to investigate sample handling and test practice before automatically rewriting a moisture model. The same account warns that historian compression can obscure important process dynamics; uncompressed data may be needed to examine transitions. If those dynamics are absent from training records, apparently strong steady-state accuracy may conceal weakness during changeovers.
An uncertainty band helps QA distinguish risk from disagreement
After aligning samples and checking the reference method, Nadia can examine the pattern of residual error. A single moisture estimate hides variation in model reliability across products and operating states. A calibrated uncertainty band, tested against independent laboratory results and difficult runs, gives more useful context than an unsupported confidence claim.
Near the limit, a central estimate cannot prove conformity; the lab still governs disposition and further confirmation may be needed. Yet a band validated in steady production may mislead after cleaning or a recipe change. That is where a sampling problem becomes a model-maintenance question.
Model drift can begin with a supplier change or a fouled dryer
The model’s relationship between inputs and moisture is learned from a particular operating history. Suppliers, formulations, cleaning and equipment condition can alter it without an obvious fault. Nadia needs to know when earlier validation no longer covers current production.
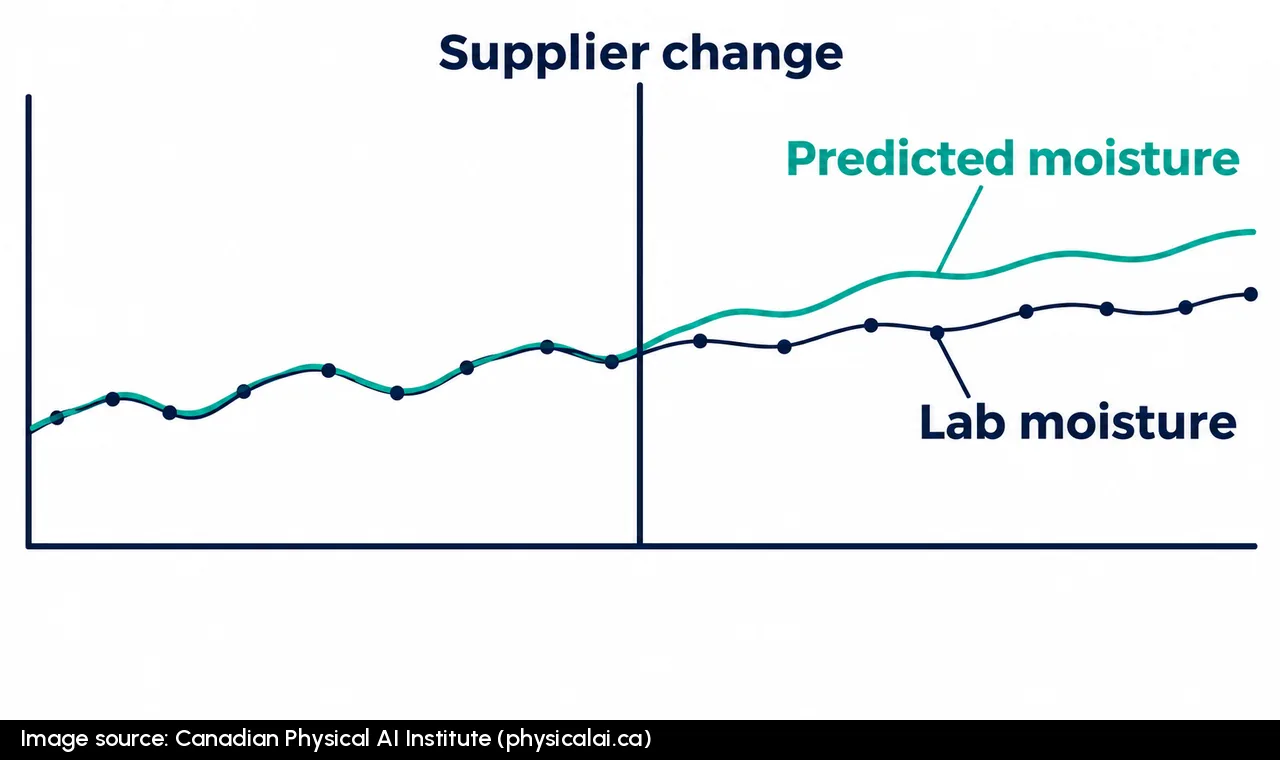
A changing process can invalidate a previously accurate relationship
The data-driven soft-sensor review describes gradual and abrupt deterioration as process conditions change. A new recipe or supplier may move the dryer into an operating region that the training data barely represents, even while the model continues to display an ordinary-looking number. The ongoing spray-drying research likewise identifies multiple formulations, frequent changeovers and sparse delayed lab observations as modelling difficulties.
New operating conditions do not prove each estimate is wrong. They do mean that performance established on earlier material may not carry over, so the model needs a way to signal unfamiliar inputs rather than silently claim the same reliability.
Paste build-up shows how a physical change can hide inside the model
A 2018 hybrid neural soft-sensor study of milk-powder drying gives a concrete example. The model estimated moisture effectively during disturbances in inlet air temperature and paste feed rate, but paste built up in the drying bed during longer operation in a way the model did not describe. Its moisture predictions then ran high.
That is research, not a quantified plant loss or commercial failure. It shows why a physical change can break an otherwise plausible relationship even when each sensor appears normal. A contaminated sensor surface creates a different failure path, so maintenance and process engineering need to diagnose the source before the estimate affects setpoints.
Drift monitoring must recognize unfamiliar operating conditions
A study presented at ADCHEM 2015 proposes watching model mismatch and multivariate process conditions to decide when updates are warranted. That links maintenance to evidence instead of an arbitrary retraining calendar. The danger of relying on normal production alone also appears in soft-sensor machine learning operations research: a model trained on normal fermentation batches deteriorated on deviating batches, with R² below 0.327 on three of ten test batches. Those were industrial-scale benchmark simulation data, not a deployed food-plant controller.
An extrapolation guard can identify input conditions outside the training and validation envelope, display the limitation and restrict what the estimate may influence. This matters because a precise-looking number is not evidence of precision in an unfamiliar operating state. Once that boundary is visible, Nadia can assign authority according to the consequences of being wrong.
Prediction authority must increase only as operating evidence improves
Engineering’s longer-term aim is automatic dryer control, but that is not the right starting responsibility for an unproven estimate. Each increase in authority creates a stronger link between prediction error and the physical product. Nadia can use four levels to distinguish observing a process from changing it.
Four authority levels separate observation from control
The progression below makes the next validation requirement explicit before the model gains permission to influence a more consequential action. QA release authority remains separate even at the highest process-control level.
| Authority level | What the model may do | Evidence needed before moving higher |
|---|---|---|
| Monitoring | Display predicted moisture and record it alongside process and laboratory data. No operating action depends on it. | Demonstrate correct sample-time alignment, reliable input data, acceptable prediction error and performance on independent batches. |
| Advisory | Warn an operator that moisture may drift or suggest a check or adjustment. The operator decides what to do. | Show useful warning lead time, manageable false alerts, reliable uncertainty bands and clear operator response rules across normal and difficult runs. |
| Operational decision support | Support a documented adjustment, hold or diversion decision under defined conditions. QA retains product release authority. | Establish QA-approved limits, sample confirmation rules, traceable decisions, out-of-range suppression and validated fallback procedures. |
| Closed-loop control | Automatically adjust permitted dryer setpoints within approved limits. Laboratory verification and QA release requirements remain in force. | Demonstrate stable control, validated operating boundaries, appropriate process response, safe failure behaviour, manual override, change control and sustained performance after model updates. |
Consequences escalate from a misleading trend to needless adjustments, incorrect disposition and continuously wrong control moves. The chemical-process practitioner account cited earlier explains why black-box neural models were often restricted to advisory use unless their predictions were constrained to follow the correct physical response. Accuracy alone cannot validate how moisture responds to a control move.
A worked moisture example shows what the margin might be worth
Nadia can illustrate the possible value without representing it as a measured result. The calculation is illustrative: every quantity and target below is hypothetical for her example plant and is not a result from any published deployment. Assume a 12.0% maximum finished moisture specification on a wet basis, with an existing target of 10.0% and a proposed target of 10.5% after variation is reduced.
With 10,000 kg of dry solids per batch held constant, finished powder mass depends on the water left in the product. The illustrative calculation uses the following relationship:
Finished powder mass = dry-solids mass ÷ (1 − moisture fraction)
At the original 10.0% target, 10,000 ÷ 0.900 = 11,111 kg of finished powder. At 10.5%, 10,000 ÷ 0.895 = 11,173 kg. Moving from 11,111 to 11,173 kg yields about 62 kg of additional mass per batch from retained water, assuming identical dry-solids output.
This is not proven saleable output or profit; specifications, customer requirements and variability still matter. Suppose the model displays an equally illustrative uncertainty band of 10.2% to 11.1%, below the 12.0% limit. It supports control only after validation through difficult conditions. If a supplier change or changeover widens it beyond the limit, the attractive average target provides no justification for automatic control.
Difficult operating periods determine whether control authority is earned
The test is not simply whether predictions match lab samples during steady runs. Start-up, shutdown, recipe changes, cleaning-in-place recovery, supplier changes and unusual feed properties all challenge the relationship, often while laboratory results lag behind the next process state. Murray Goulburn’s hourly checks illustrate continuing verification, not a universally sufficient sampling frequency.
Nadia’s plant needs its own evidence for when checks are taken and when automatic control can remain active. Critical input loss, excessive uncertainty or extrapolation calls for conventional operation. Our guide to AI pilot readiness discusses why fallback and failure responsibility belong in the deployment design. Laboratory feedback can then improve the model, but not by treating every difference as a reason to alter it.
Laboratory feedback should correct persistent bias without chasing random error
Physical samples keep the estimate connected to the product, yet each laboratory result also contains variation. Recalibrating after every mismatch risks teaching the model to follow random noise. Persistent offset and changed process relationships need different remedies.
Bias correction begins with the right historical prediction
The inferential-monitoring guidance cited earlier compares each laboratory result with the model’s historical prediction for the same sample time. Tracking the laboratory value minus that prediction reveals whether errors alternate or continue in one direction. Its cumulative sum method, or CUSUM, produces an irregular pattern when positive and negative errors roughly balance, while a sustained slope indicates persistent bias.
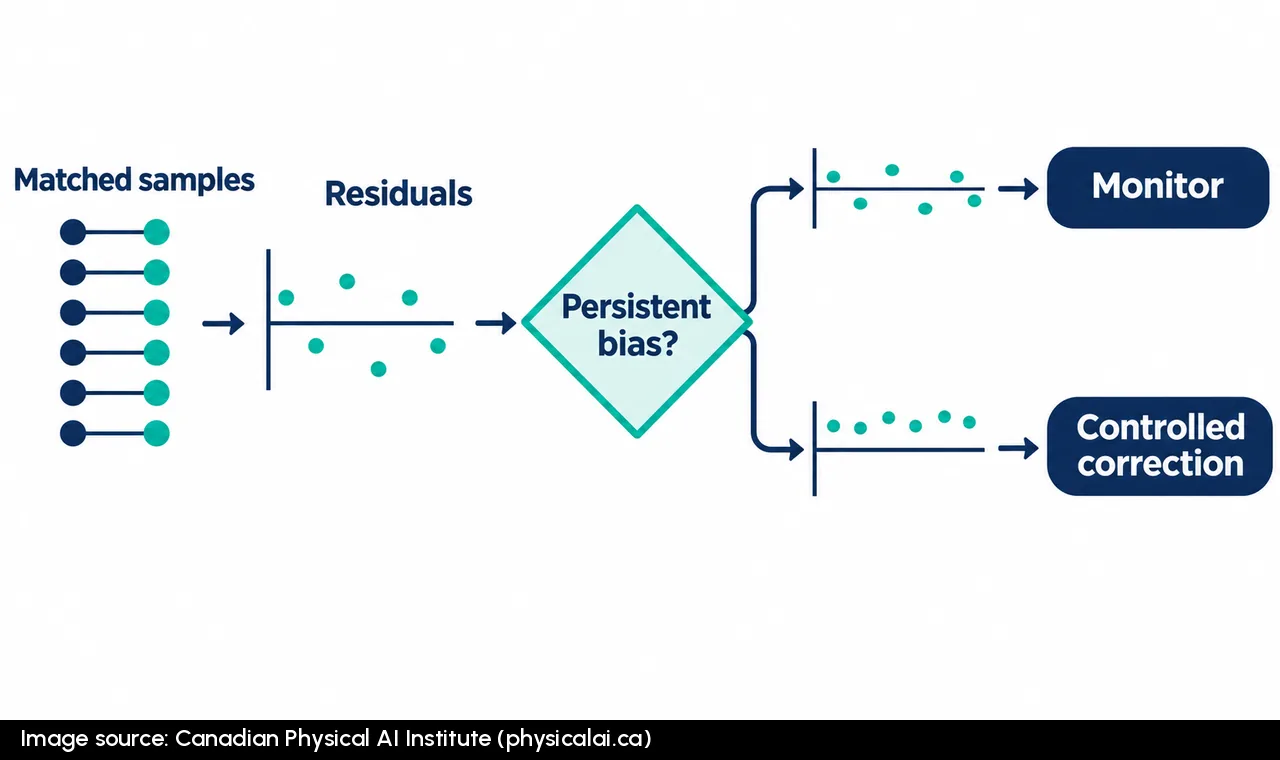
The worked practitioner example calculated a correction from the last six laboratory records instead of reacting to each sample. Six is not a universal window; repeatability, transitions and correction risk determine the choice. An isolated disagreement may deserve investigation without immediately modifying the estimate.
Re-biasing and retraining solve different problems
When the relationship remains valid but predictions stay consistently high or low, controlled bias correction may suffice. Changed recipes, feed characteristics or process behaviour can require fresh reference data and retraining instead. A review of adaptive soft-sensor methods describes moving windows, recursive adaptation and model ensembles: one changes the weight of historical observations, another updates parameters as data arrives, and ensembles combine models.
These methods are not interchangeable. The ADCHEM study cited earlier cautions that poor moving-window sizes or update intervals can chase noise or respond too slowly to genuine drift. Until a revised model passes validation, retaining the previous approved version gives the plant a defined rollback option.
Each model update needs a documented owner
That separation requires explicit responsibilities. QA owns the reference method and lab-use rules; engineering or a model specialist diagnoses and tests updates; operations responds to predictions; and maintenance maintains the instruments providing inputs. Supplier, recipe and packaging changes need an assigned reviewer who decides whether the target, data or process context has shifted enough to require new validation.
The update record links the original version, reference data, reason for change, tests, approval and rollback method. Without it, a model accepted at commissioning could change in ways QA never reviewed. This accountability also shapes the purchasing choice.
Choosing an AI soft sensor solution determines who owns the operating risk
Building an estimator internally, purchasing a specialized platform and extending existing advanced process control are all possible routes. The choice also determines outage resilience, data access and maintainability. Her purchasing criteria follow from the operating risks.
The three routes have different weaknesses
Each approach needs a different starting capability and exposes a different weakness after commissioning. Demonstration accuracy alone cannot settle the choice.
| Solution route | What the plant needs to provide | Where the approach can break |
|---|---|---|
| Build in-house | Process knowledge, accessible historical data, modelling skills, an on-site runtime, integration engineering, validation and ongoing maintenance ownership. | The model may work technically but become unsupported when specialists leave, recipes change or plant systems are updated. |
| Buy a soft-sensor platform | Clear use case, validated laboratory data, integration access, QA acceptance, contractual data rights and an accountable internal owner. | The plant may depend on external support, restricted model access, cloud connectivity or proprietary formats that complicate maintenance and vendor exit. |
| Extend existing advanced process control (APC) | Suitable control infrastructure, process engineering support, reliable automation interfaces and a validated way to connect prediction with control response. | A good quality estimate may still produce poor control if the process response is misunderstood, operating constraints change or the controller cannot safely handle uncertainty. |
No route wins universally. In-house development fits a plant able to sustain modelling and integration skills; a platform may suit one seeking packaged support; and an APC extension may fit established control infrastructure. The test is sustained operation through production changes.
Local operation and model ownership protect production continuity
An external network or service outage need not remove the estimate if its runtime and required inputs are local. A vendor-reported Emmi case study describes site-server software connected to automation through OPC, adjusting existing control-loop setpoints across a broad product portfolio. That demonstrates integration, not universal resilience or cybersecurity.
Nadia needs a clear distinction between losing external connectivity and losing essential local sensor data. The latter makes a reliable estimate impossible and calls for the approved fallback. Export rights to raw process data, lab references, training sets and the trained model enable independent testing, rebuilding and migration. Contracts can prohibit vendor cloud collection or secondary training without consent, protecting sensitive supplier and formulation data. A local installation without those rights can still create provider dependence.
Changes after commissioning need approval and rollback
Support arrangements need to specify who identifies drift, collects new samples, retrains the model and approves deployment. Automated adaptation may help, but a change affecting setpoints or product disposition still needs QA and engineering review. Nadia needs to compare a proposed version against the approved one on difficult conditions and reject regressions.
If an update misbehaves, a tested rollback restores the prior approved model without waiting for external intervention. Records also need to identify the model version and bias-correction method behind each significant operating decision. The soft-sensor review cited earlier notes both the cost of manual maintenance and the historical absence of automated maintenance in many systems. A promise of continuous improvement shifts maintenance work; it does not eliminate its cost or the need to verify results.
The model should show its reasoning and recognize its limits
Staff need more than a moisture number to investigate a prediction. Displaying the contributions of current dryer conditions, feed characteristics and recent history can indicate which inputs deserve attention, although such contributions do not prove causation. The same interface can show prediction uncertainty, operation outside the validated envelope and checks against plausible process behaviour.
When those checks fail, higher-risk authority can be suppressed rather than leaving an implausible estimate active. Closed-loop use additionally depends on proving that the controller responds in the physically correct direction and magnitude. This visibility helps contain errors before a control move.
Lifetime support cost can outweigh the initial modelling expense
Internal builds need continuing specialist and integration capacity; platforms may bring subscriptions, support fees and paid changes; APC extensions need both model and controller expertise. All three still consume laboratory sampling, input-instrument maintenance, validation and fault investigation. Those recurring obligations belong in the cost model.
A useful lifetime comparison covers response to faults, support availability, updates, training, integration changes, export rights and the cost of vendor exit. Our guide to choosing a Physical AI integrator explores these questions for Canadian food plants. Next comes the boundary around product disposition.
A prediction used for product disposition becomes part of the control record
Using an estimate to suggest an operating adjustment differs from using it to hold, divert or release powder. The second use affects documented product conformity, so the prediction and any response need to fit the plant’s established control system. AI itself carries no automatic approval.
Canadian preventive control requirements apply to the decision
The Canadian Food Inspection Agency’s monitoring procedures guidance addresses what is monitored, how often, by whom and through which records. Its verification procedures guidance covers how the business checks that preventive controls and monitoring operate as intended. For businesses subject to the requirements, section 89 of the Safe Food for Canadians Regulations addresses plan contents including critical control points, limits, monitoring, corrective actions, verification and supporting evidence.
We found no CFIA guidance specific to AI soft sensors. Software presence is not regulatory approval or permission to replace a monitoring method. If a prediction influences a critical control point or a formal disposition decision, Nadia needs to place that use within the applicable documented monitoring and verification arrangements.
A quality prediction should not quietly become a release method
At pilot stage, the moisture estimate can inform process quality while laboratory testing continues to govern release. Any later role in holding, diverting or releasing product requires defined QA-approved procedures. The record needs the predicted value and time, product identity, model version, input status, uncertainty or out-of-range signal, applicable limit, operator or automatic response and subsequent laboratory verification.
For a disputed result, it also preserves sample details, applied correction and final QA disposition; when the model fails, the procedure identifies a fallback. Not every moisture prediction measures a critical control point, and the plant first determines the variable’s actual safety and quality role. Bounded automatic dryer control and finished-product release can remain separate, allowing a credible route to operational benefit without implying a new regulatory approval.
Financial return depends on earlier useful decisions, not prediction accuracy alone
The investment case turns on whether earlier information changes outcomes while the product can still be influenced. Average prediction error cannot establish recovered moisture or throughput. Nadia can connect the model’s record to plant decisions and the resulting compliant production.
Decision lead time measures the opportunity to intervene
Potential lead time is the interval between a useful prediction and when the corresponding laboratory result ordinarily reaches the decision-maker. Actual intervention time matters more: a warning may be early relative to the lab yet too late for the affected powder. Conversely, even a small time advantage can matter near the point after which rework or diversion is unavoidable.
The golden batch timeline allows Nadia to compare detection, operator response and the material that response could influence. Counting warnings without that connection overstates operational value. The value lies in the intervention, not the timestamp alone.
Alert usefulness measures whether operators can trust the information
Warning outcomes can be classified as appropriate action, appropriate inaction, unnecessary response or missed quality event. That matters especially during ordinary moisture fluctuations. Frequent false warnings can erode attention, while a somewhat less accurate model might still identify consequential movement toward a limit in time to help.
The errors have unequal costs: unnecessary adjustments consume effort, whereas missed high-moisture conditions can affect product quality and disposition. Alert performance needs checking across steady operation, starts, supplier changes, changeovers and cleaning recovery. The chemical-process account cited earlier emphasizes operator confidence as essential to sustained use. Recorded actions and missed events show whether the model is earning that confidence rather than merely displaying plausible values.
Moisture recovery and throughput need separate financial accounting
The illustrative mass calculation identifies water potentially retained at a higher target, but only compliant finished product can establish a realized gain. Dryer throughput, variability, energy, holds, rework and cleaning may also change, and the accounting needs to distinguish them. In particular, increased powder mass from retained water and capacity used for greater production cannot be counted twice as the same benefit.
The dryer cases do not forecast her return. Her evaluation compares incremental compliant output and verified savings with integration, lab checks, model support and maintenance, while also recording unnecessary actions, additional holds and any greater off-spec risk. QA and operations can then reconstruct return from the same records.
The next supplier season remains the difficult test
Nadia can begin with a monitored estimate, verify it against correctly timed laboratory results and introduce advisory warnings once their uncertainty and operating usefulness are established. Evidence through difficult conditions may justify documented adjustments and eventually bounded closed-loop control, while laboratory methods retain their approved role in product disposition. That progression makes a narrower moisture margin possible without treating a prediction as a release certificate.
The harder test comes after new suppliers, recipes, cleaning cycles and operating states that were scarce in the training history. Extra powder mass and earlier decisions may become measurable soon after commissioning, but a full season is needed to challenge the apparent stability of the model’s uncertainty band. A precise displayed number can survive long after the process relationship supporting it has changed. When the dryer operates closer to its moisture limit, there is less room to discover that error late.